The water pump is the most critical component in a cat water fountain. Its quality determines noise level, reliability, and product lifespan. Here’s how quality manufacturers test fountain pumps.
Individual pump testing
Quality manufacturers test every pump individually — not just samples from a batch. Each pump undergoes:
Flow rate testing
Measuring actual water flow against specified flow rates (typically 100-300 L/hour for cat fountains). Pumps that don’t meet flow specifications are rejected.
Noise level testing
Using calibrated decibel meters to verify noise levels below 35dB. Pumps that exceed noise specifications are rejected. HS Smart Pet tests every pump for noise level.
Power consumption testing
Verifying that power consumption stays within specified wattage (typically 1.5-2.5W). Excessive power consumption indicates motor inefficiency or defects.
Start-up testing
Testing that pumps start reliably in all orientations and water levels. Pumps that fail to start consistently are rejected.
Waterproof integrity
Verifying that waterproof seals prevent water ingress into the motor chamber. Failed seals mean rejected pumps.
Burn-in testing
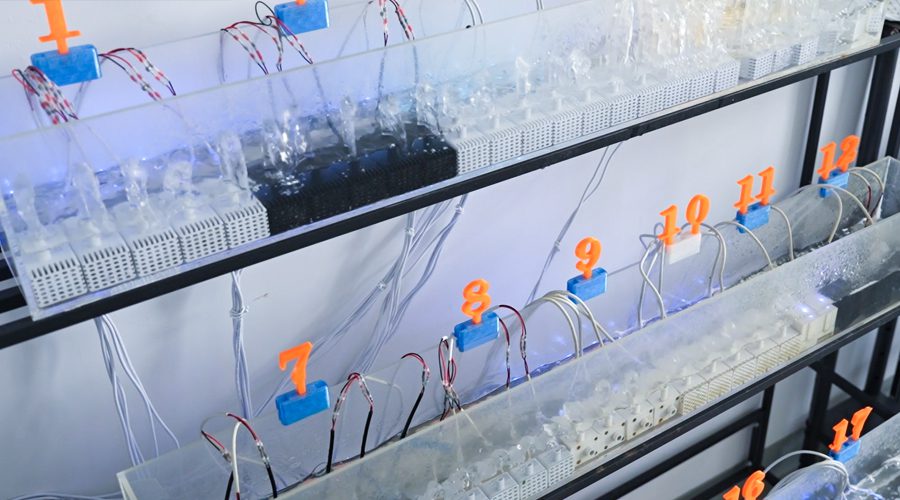
Burn-in testing is the most important quality gate for fountain pumps:
Duration: Pumps run continuously for 48-72 hours (some manufacturers run longer).
Purpose: Identifies early failures that would otherwise reach customers. Most pump failures follow a bathtub curve — occurring either very early (manufacturing defects) or very late (wear-out). Burn-in catches early failures.
Monitoring: During burn-in, flow rate, noise level, and power consumption are monitored for consistency. Pumps that show performance degradation during burn-in are identified and investigated.
Environment: Burn-in typically happens in dedicated testing areas with monitoring equipment.
Statistical process control
Beyond individual testing, quality manufacturers track pump performance data:
Flow rate distribution — Ensuring consistency across production batches.
Noise level trends — Identifying gradual quality drift before it becomes a problem.
Failure rate tracking — Monitoring defect rates and investigating root causes.
Batch comparison — Comparing performance across production batches to identify variations.
What separates quality testing
100% testing vs sampling. Testing every pump versus sampling from a batch makes a significant difference in quality assurance.
Dedicated burn-in facilities. Purpose-built burn-in areas with monitoring equipment indicate serious quality commitment.
Calibrated equipment. Test equipment must be calibrated regularly to maintain accuracy.
Data recording. Recording test results for every pump enables traceability and trend analysis.
The bottom line
Pump testing is the foundation of fountain quality. Manufacturers who test every pump individually, conduct burn-in testing, and track performance data deliver more reliable products.